The Yellow Tape Cult: Why We Fundamentally Do Not “Implement Lean Manufacturing”
Smbat Dzhanunts, founder of Hattatsu Group · November 3, 2026 · 7 min read
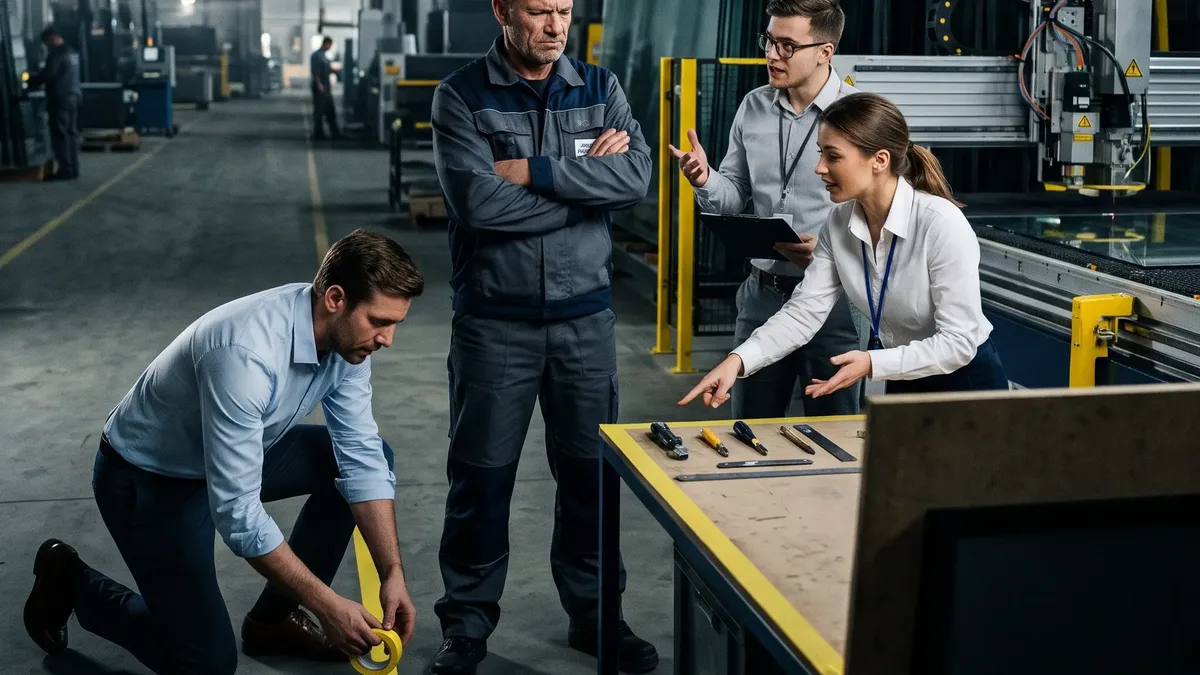
Yellow warning tape on concrete and tool outlines on workbenches will not save a plant from cash gaps and missed deliveries. We look at why the market is full of sellers of quick and cheap “lean manufacturing”.
Every other plant owner sighs heavily at the words “lean manufacturing”. People have developed a persistent skepticism, and I understand these entrepreneurs perfectly well.
Where did this come from? The reason is simple: business always wants results fast, easily and preferably cheaply. The market instantly responded to this weakness with an army of consultants ready to feed the illusion.
Their script is the same everywhere. Cheerful people with sticky notes and rolls of warning tape walk into a company with revenue close to a billion rubles. In all seriousness, they explain to a top-grade fitter and to a shop manager with thirty years of experience how to put down a wrench properly and at what angle to stand a broom. Then come the round dances around 5S boards, posters with Japanese characters on the walls and morning meetings with mantras about fighting waste.
On our projects we also use floor marking, workstation standardization, 6S and waste reduction. There is nothing wrong with these tools as such, they are normal basic shop-floor hygiene. The problem is different: the outward signs of order started being sold as a ready-made business transformation.
Six months pass. The plant has spent its consulting budget, covered the whole shop in yellow tape and filled terabytes of spreadsheets. The owner opens the cash flow statement and sees zero. Profit has not grown. Orders are late just as before. But the machine operator now has a perfect screwdriver outline painted on his workbench, and he has no idea why.
Because a real rebuild of a production system is never fast. It was never about tape or nice posters on the walls. And the attempt to solve systemic problems with cheap cosmetics gave rise to a cargo cult and an imitation of frantic activity.
A scientific dead end: why local fuss on the shop floor hurts the business
What most of these specialists do is called suboptimization in systems theory and cybernetics. The law of systems engineering is simple: maximizing the efficiency of a single element almost always reduces the efficiency of the system as a whole.
A plant is not a single lathe workstation or a cutting table. A company is a complex dynamic system of interconnected loops:
- The owner’s strategy and financial model.
- Sales plan and commercial policy.
- Raw material procurement and inventory management.
- Production flow and capacity balancing.
- In-plant logistics and the customer shipping schedule.
When consultants rush to bring order to a single machine in isolation from the rest of the system, they only speed up the generation of problems.
A classic example from our audits of glass and window production. The glass cutting area was optimized. Zones were marked out, operators were trained to change tooling quickly, cycle time was reduced. The shop manager is happy, the machine runs nonstop, and workers cheerfully cut square meters for their piece-rate bonus.
Except that at this very moment the sales department is selling insulated glass units of non-standard sizes, for which the right spacer frame is not in stock. And the tempering furnace next in line physically cannot take that volume of raw glass.
The outcome of this “leanness” is sad. The whole aisle was stacked with pyramids of cut glass worth tens of millions of rubles. The blanks sat for weeks, gathering shop dust, workers bumped them with forklifts and broke them when moving them around. The local speed-up at cutting led to frozen working capital, more defects and paralyzed in-plant logistics.
Why we design the system architecture instead of “implementing lean manufacturing”
We at Hattatsu Group categorically do not do isolated “lean implementation”. Lean or TPS tools (be it SMED quick changeover, 6S workstations or Poka-Yoke error-proofing) are simply a fitter’s tools. They are the wrenches in an engineer’s toolbox.
It makes no sense to hire a team of experts just to have them show you how to hold an adjustable wrench. Professionals build the architecture of a production system in which every element serves the shareholder’s single goal.
If a company has no end-to-end management loop, any lean tool turns into a waste of budget. Before approaching the machines, you need to synchronize the directors’ offices with the shop floor.
For this, international manufacturing practice uses Hoshin Kanri (policy deployment) or its equivalents.
Hoshin Kanri: how to connect an investor’s ambitions with a worker’s hands
Hoshin Kanri translates as “direction compass”. The method links the owner’s top-level financial requirements with the shift and daily task of a specific foreman.
The link is built through an end-to-end matrix. It does not allow a single improvement to be launched on the shop floor unless it is consistent with four levels:
- The owner’s strategic goal. For example, increasing operating profit and EBITDA by 20-35% without buying new equipment (Zero CAPEX).
- Annual management goals. Higher overall equipment effectiveness (OEE) at bottlenecks and faster capital turnover.
- Cross-functional tasks. An agreed set of rules between sales, procurement and production.
- Shift KPIs in the SEQCDDM loop: safety, quality, cost, development, logistics, people.
To make this structure work without sabotage, the Catchball principle is used. Strategy is not sent down as a blind order. The board throws the ball with target benchmarks to department heads. The production manager passes it back with a calculation of the shop’s technological constraints. The commercial director adjusts contracting rules to the production rhythm.
The result is a firm horizontal agreement. After that, the shop stops producing semi-finished goods for the sake of a nice report and starts making products strictly at the pace of customer payments.
A checklist for the plant owner: what to ask the team before starting
If you are planning a production system development project with external experts, ask them four practical questions. Their answers will quickly show who you are dealing with: system architects or sellers of quick cosmetic fixes.
- “How do changes in a specific area fit with the sales plan and raw material supply?”Optimization in isolation from sales and procurement is pointless. If the experts are not interested in the order structure, shipping rhythm and raw material constraints, the shop will simply start making blanks for the warehouse faster.
- “How exactly is training organized on the shop floor, and how do you lock in the changes?”Training hours and work with people are vital. Without involving foremen and operators, no system will take root. But training should not be a lecture in a classroom detached from real life. Theory has to turn straight into work standards at specific workstations, and skills have to be reinforced through practice and clear shift metrics.
- “How do you deal with the company’s main constraint?”At any given moment every plant has only one or two key bottlenecks that limit total output. Spending the team’s effort and time on improving areas outside this bottleneck gives the business no increase in finished goods.
- “Are you ready to share risks with us and tie part of your fee to the results of the year or quarter?”Professional teams understand that rebuilding a production system takes time and joint work. A healthy model of cooperation is a partnership: a basic monthly fee for the experts’ field work plus a bonus at the end of the period for reaching agreed measurable targets or reducing production cost. Those who came just to sell a process and stick tape on the floor will never share risks with the owner.
Business does not need nice reports about lines painted on the floor. The owner needs a stable, manageable system where people are trained, sales are synchronized with the shop floor and output grows on existing capacity.
You can assess the maturity of your company’s operating system and see the real areas of hidden losses through our online diagnostics.
The principles of end-to-end flow synchronization, the Hoshin Kanri matrix and shop-floor engineering metrics are explained in our industry glossary.
More breakdowns in our Telegram channel.
Get in touch with our representative directly
Choose the way that suits you - write or call us directly.